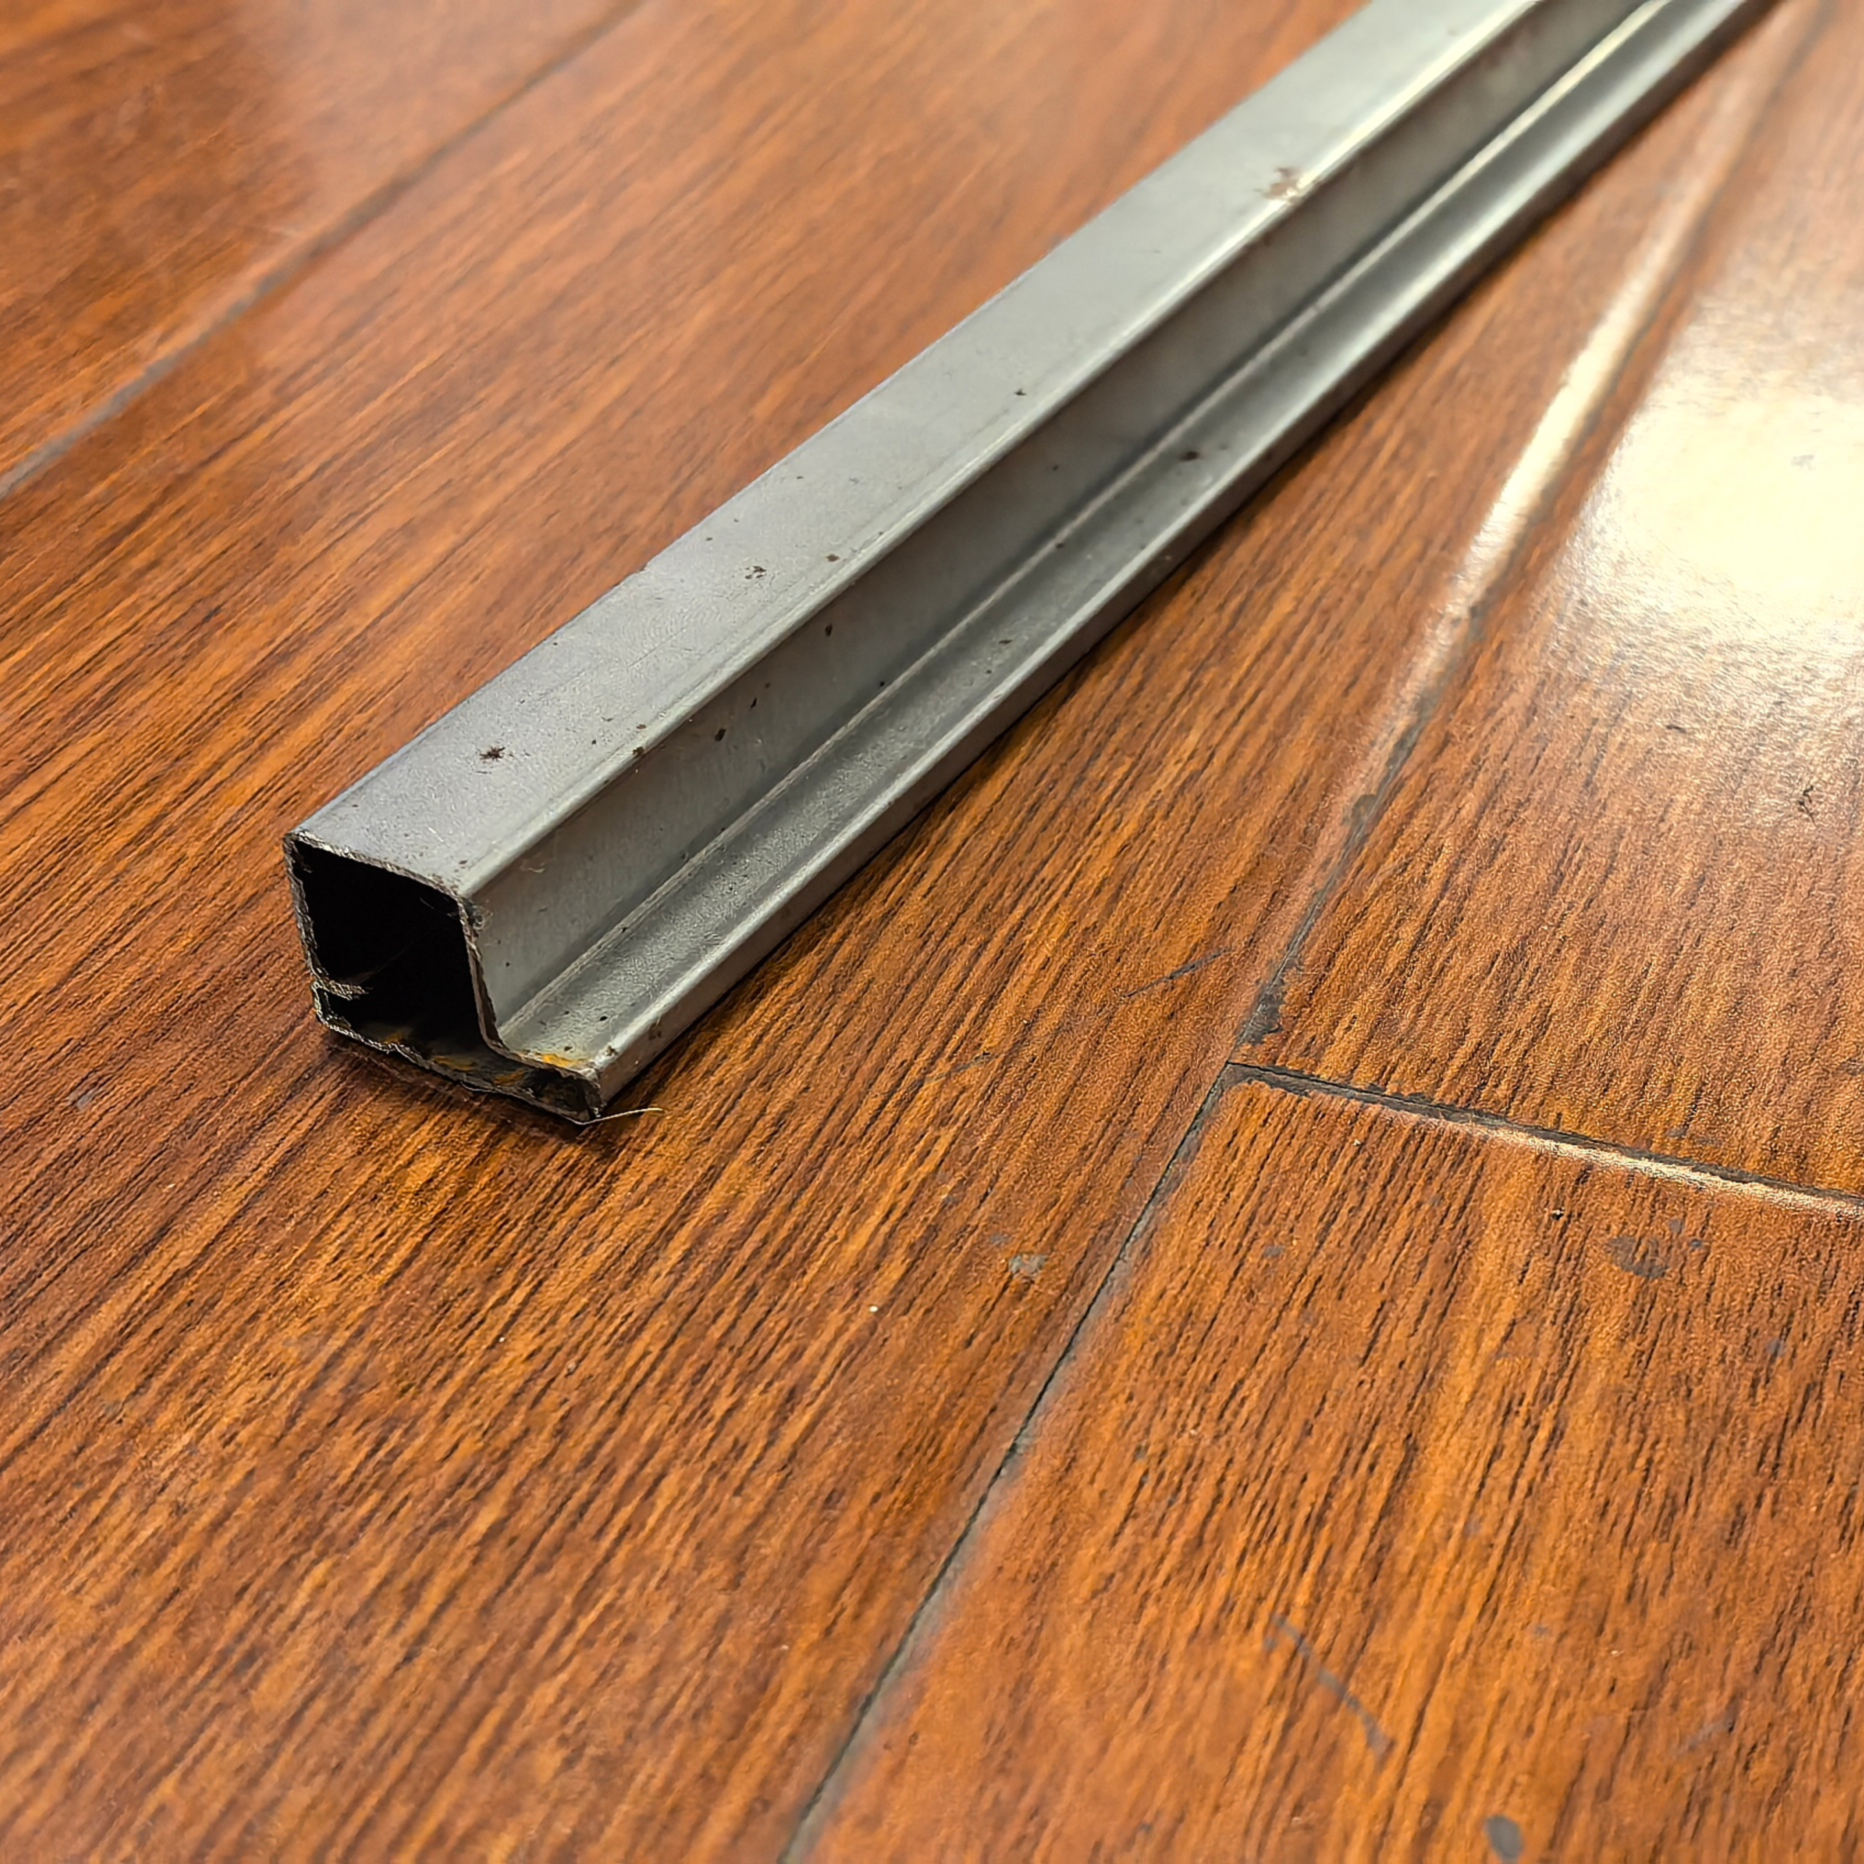
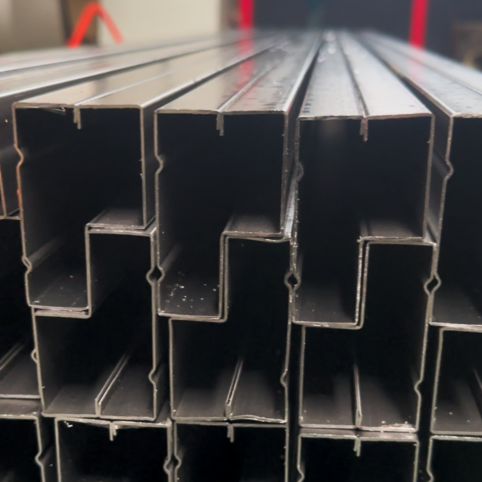
Seam‑Welded P‑Shaped Column Rolling Machining Equipment for Heavy‑Duty Storage Racks

This roll forming line produces seam‑welded P‑shaped uprights for heavy‑duty pallet racks and industrial storage systems. The machine forms a P‑section from flat strip, then continuously welds the closed edge using high‑frequency induction welding (HFIW). Post‑weld stations remove burr, cool, and size the profile. Integrated servo punching creates teardrop or diamond holes. Material thickness 0.5‑2.5mm, line speed 8‑12 m/min. Ideal for rack manufacturers requiring extra‑strong, closed‑section uprights with superior torsional rigidity.

Brand: SAVANY
Machine Type: Roll forming machine / Press brake / Custom production line
Color: Custom / Customizable
Capabilities: Roll forming, punching, shearing
Roll Forming Material: SPCC/SPCD/SPCE/SGCC/CGCC/304/5052
Profile Dimensions: Custom
Customization Level:100% custom
Payment Terms: T/T
Lead Time: 90 working days
Place of Origin: Guangdong, China

In‑Line Weld P‑Beam Pallet Rack Upright Cold Rolling Machines

– Ultra‑Strong Closed‑Section Columns for Heavy Loads

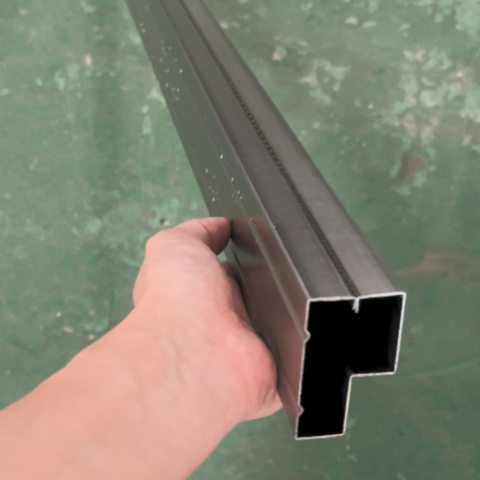
The in‑line welded P‑beam pallet rack upright roll forming machine is a specialized line for manufacturing seam‑welded P‑shaped columns used in heavy‑duty pallet racks, drive‑in racks, and seismic‑rated storage systems. Unlike open C‑channel or roll‑formed P‑beams, the welded P‑section has a fully closed edge, providing exceptional torsional rigidity and load capacity.

Why choose welded P‑beam uprights?

Welded P‑beams combine the strength of a closed tube with the convenient shape of a P‑section. The welded seam creates a continuous, uniform wall thickness, eliminating weak points. These uprights are ideal for high‑bay warehouses, seismic zones, and applications requiring maximum strength‑to‑weight ratio.

Production process:

  1. Uncoiling – Hydraulic uncoiler (10‑20 tons), coil width up to 450mm.
  2. Straightening – Leveling rolls ensure flat material.
  3. Servo punching – Creates teardrop or diamond holes for beam connectors, plus base plate mounting holes. Programmable patterns.
  4. Pre‑forming – Initial bending of the flat strip into a pre‑closed P shape (open seam).
  5. High‑frequency induction welding (HFIW) – A coil induces current to heat the seam edges; squeeze rolls forge them together without filler metal. This produces a continuous, strong weld.
  6. Burr removal – A scraper removes internal and external weld flash.
  7. Sizing & straightening – Final calibration ensures perfect shape and straightness.
  8. Post‑weld annealing (optional) – Reduces residual stress for critical applications.
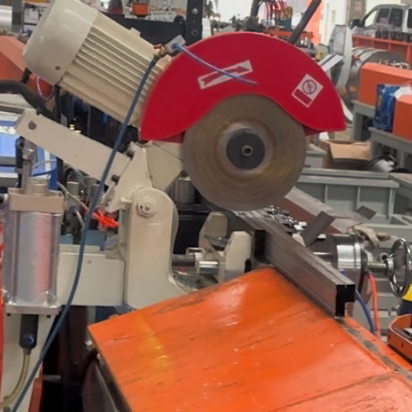
  9. Cut‑off – Flying shear cuts to exact upright length (±0.5mm).
  10. Stacking – Optional automatic stacker.

Key features:

Material specifications:

Typical P‑beam sizes:

ParameterRange
Overall width60‑120 mm
Overall depth40‑80 mm
Material thickness0.5‑2.5 mm
Line speed8‑12 m/min
Punching accuracy±0.3 mm
Cut‑off tolerance±0.5 mm
Main power50‑80 kW (including welder)

Applications:

Optional features:

Included services:

Lead time: 90-120 working days (due to welder integration).


    ➤