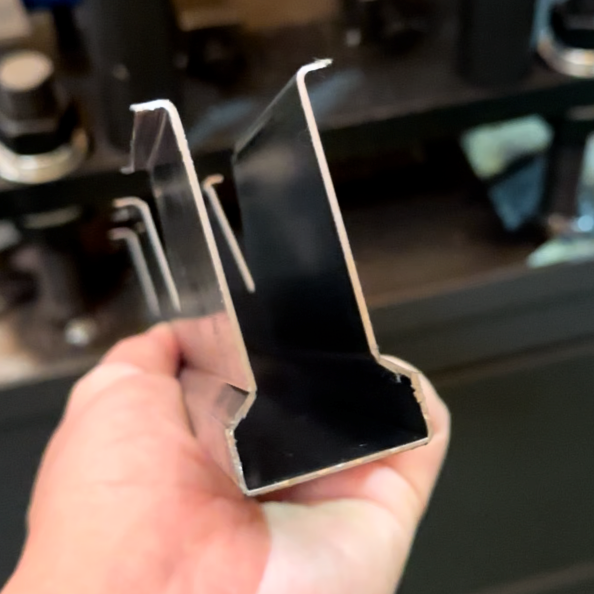
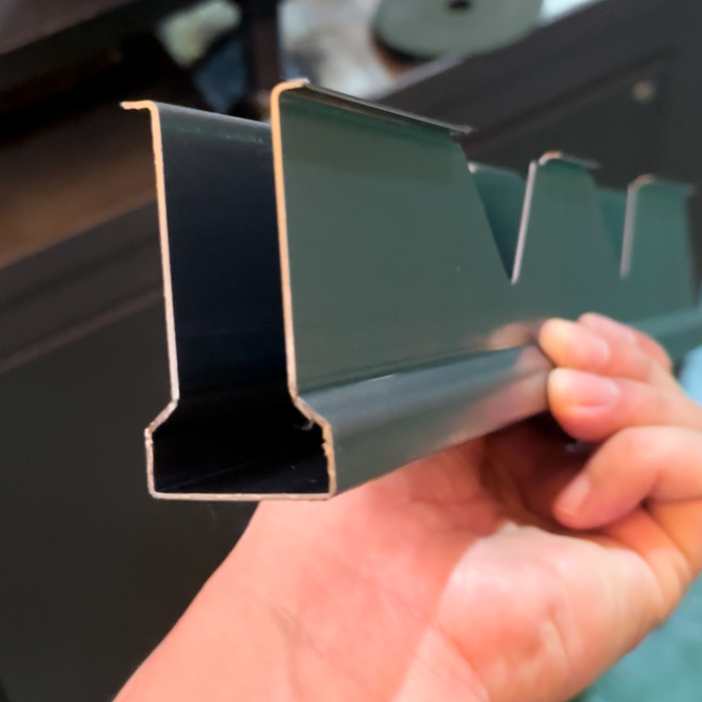
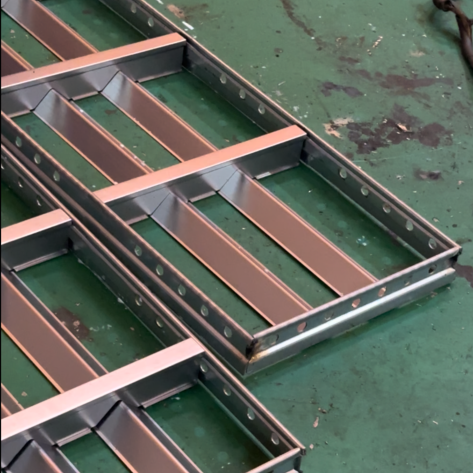
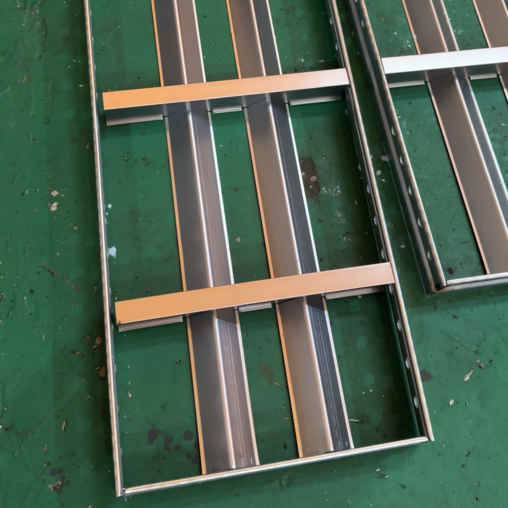
Tooth‑Pattern U‑Channel Concrete Formwork Beam Production Line

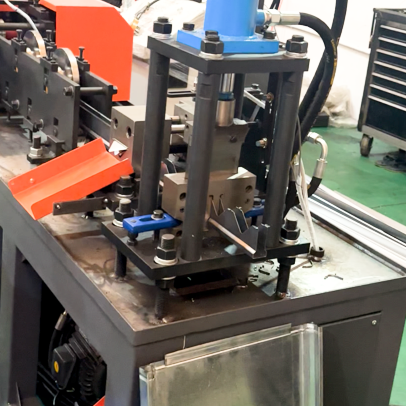
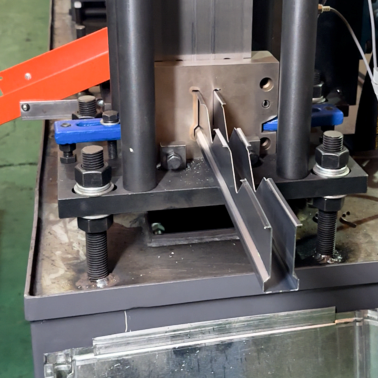
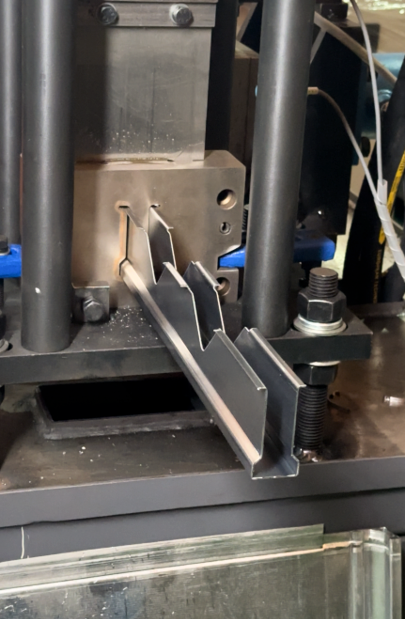
This roll forming system produces serrated (toothed) U‑beams used as load‑bearing horizontal members in concrete slab formwork systems. The teeth along the top flange provide positive grip for wooden planks or steel decking, preventing slipping. The machine forms 2‑3.5mm galvanized steel coil into U‑profiles with precision‑rolled tooth patterns. Inline punching creates end connector holes and tie rod slots. Speeds up to 6 m/min, cut‑off tolerance ±1mm. Ideal for formwork manufacturers supplying high‑load slab formwork for bridges, high‑rises, and industrial floors.

Brand: SAVANY
Machine Type: Roll forming machine / Press brake / Custom production line
Color: Custom / Customizable
Capabilities: Roll forming, punching, shearing
Roll Forming Material: SPCC/SPCD/SPCE/SGCC/CGCC/304/5052
Profile Dimensions: Custom
Customization Level:100% custom
Payment Terms: T/T
Lead Time: 90 working days
Place of Origin: Guangdong, China

Serrated U‑Beam Formwork Roll machining Equipment

– High‑Grip Support Beams for Concrete Slabs

The serrated U‑beam formwork roll former is a specialized line for manufacturing U‑shaped steel beams with serrated (toothed) top flanges. These beams are used as primary or secondary supports in concrete slab formwork systems. The teeth bite into wooden planks or steel decking, eliminating the need for additional fasteners and reducing assembly time.

Why serrated U‑beams?

Traditional smooth U‑beams require screws or clamps to hold decking, which is labor‑intensive and can damage the formwork. The serrated pattern provides a mechanical lock, allowing quick placement and removal of planks. The teeth are roll‑formed, not cut, preserving material strength.

Production process:

  1. Uncoiling – Heavy‑duty uncoiler (10‑15 tons), coil width 300‑500mm.
  2. Straightening – Leveling rolls.
  3. Tooth rolling – Special roller dies emboss the serrated pattern (teeth) onto the top flange. Tooth pitch and height are customizable.
  4. Servo punching – Creates end connector holes, tie rod slots, and lifting eye holes.
  5. Roll forming – 10‑12 passes form the U‑shape. Rollers Cr12MoV, HRC58‑62.
  6. Cut‑off – Flying shear cuts to length (±1mm).
  7. Stacking – Powered stacker.

Key features:

Material range:

Typical side frame specifications:

ParameterRange
Beam width100‑200 mm
Beam height50‑80 mm
Material thickness2‑3.5 mm
Tooth pitch20‑40 mm
Tooth height1‑2 mm
Line speed5‑8 m/min
Cut‑off tolerance±1 mm

Applications:

Optional features:

Included services:

Lead time: 75‑90 working days.


    ➤